

Minerals & Fertilizers
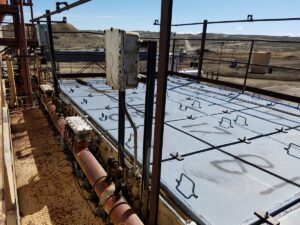
Minerals and fertilizer production is not only critical for every aspect of modern life, it is also very prevalent in the intermountain west and we have extensive experience handling salt, sulfate of Potash, soda ash, calcium products, clays, and other products. Our typical scope of processing equipment in these facilities includes heavy duty drag conveyors, bucket elevators, screw conveyors, bulk bag handling, dust collection equipment, truck & rail loading systems, magnets, fluid bed dryers & coolers, screeners, vibratory feeders, and storage silos.
View our “Minerals & Fertilizers” case studies below.
What we do for minerals and fertilizer plants
We handle salt, sulfate of potash, soda ash, calcium products, clays and gilsonite. These plants crush, dry, screen, convey and load abrasive material at high rates. One drag conveyor we supplied to a Utah plant has moved more than 540,000 tons of mineral in over ten years.
Typical equipment
- Drag conveyors and bucket elevators from CDM Systems and Sidney Manufacturing
- Screw conveyors from KWS
- Cage mills and impact crushers from Stedman, and jaw and roll crushers from Sturtevant
- Fluid bed dryers and coolers from Carrier, and rotary dryers from Heyl & Patterson
- Screeners from Rotex
- Dust collectors from SLY
- Railcar unloading from Cyclonaire and loading spouts from Vortex
The case studies below come from a Utah mineral plant.